Blow-Up Ratio: Essential Guide to Blown Film Extrusion and Quality
What Is Blow-Up Ratio?
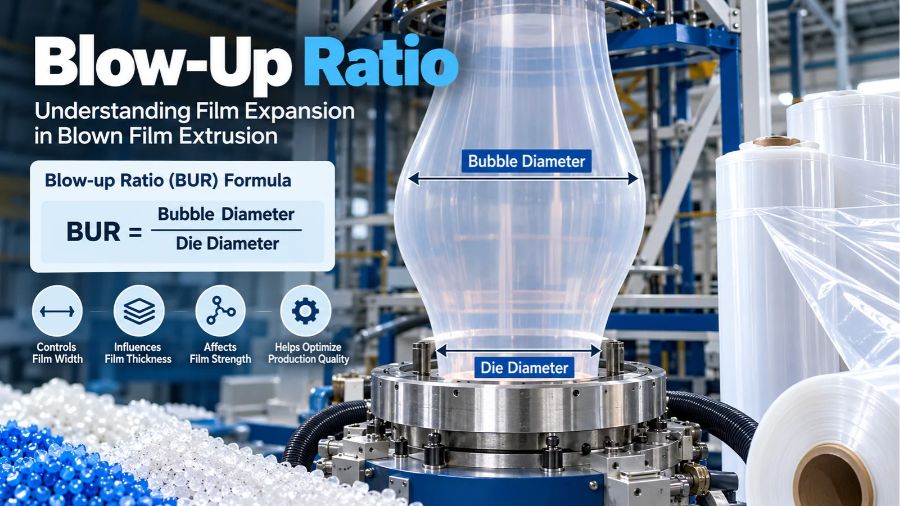
The blow-up ratio (BUR) is the ratio between the diameter of an inflated plastic film bubble and the diameter of the circular extrusion die through which the molten polymer passes. It measures the extent of expansion in the transverse direction, which is perpendicular to the film’s length. Manufacturers use this measurement to understand how the film is stretched during production and to help determine the dimensions and properties of the finished material. For example, a blow-up ratio of 2:1 means the bubble diameter is twice the die diameter. A higher ratio indicates greater transverse expansion, although it does not automatically mean that the finished film will have better overall quality.
How Does the Blow-Up Ratio Work?
The blow-up ratio is established during the blown film extrusion process, in which plastic resin is melted, forced through a circular die, inflated with air, cooled, and collected as a continuous film. The molten polymer initially emerges as a tube with a diameter determined largely by the die geometry. Air introduced inside the tube expands it into a larger bubble while the material remains soft enough to stretch. As the bubble cools, the polymer solidifies and retains its final tubular dimensions. The relationship between the original die diameter and the expanded bubble diameter provides the blow-up ratio, helping operators understand the amount of transverse stretching applied during film formation.
The Role of the Extrusion Die
The extrusion die is the circular opening through which molten plastic leaves the extruder. Its diameter establishes the reference dimension used to calculate the blow-up ratio. A smaller die can produce a wider bubble when paired with an appropriate expansion ratio, while a larger die can produce a similar bubble diameter at a lower ratio. However, the die also affects melt flow, output capacity, pressure, and the stability of the extruded tube. Consequently, manufacturers must consider die design alongside polymer characteristics and production requirements rather than selecting a die based solely on the desired ratio.
How Air Pressure Expands the Film Bubble
Air trapped inside the extruded tube creates the pressure needed to expand the molten polymer. Operators control the bubble diameter by managing the internal air volume, while cooling air and haul-off equipment help stabilize the expanding film. The bubble must remain sufficiently stable for the film to cool evenly and maintain its intended dimensions. Excessive expansion or poor air distribution can contribute to bubble movement, uneven thickness, and wrinkles. The relationship between air supply, melt strength, cooling conditions, and haul-off speed is therefore essential to maintaining a consistent blow-up ratio throughout production.
Blow-Up Ratio Formula and Calculation
The standard formula for calculating the blow-up ratio is straightforward: divide the inflated bubble diameter by the extrusion die diameter. Both measurements must use the same units, such as millimeters or centimeters. The result is expressed as a ratio, commonly written as 2:1, 2.5:1, or 3:1. The calculation describes transverse expansion rather than the complete stretching history of the film, because the material is also stretched in the machine direction as it is pulled away from the die. For accurate process analysis, the blow-up ratio should therefore be considered alongside film thickness, haul-off speed, and other operating parameters.
Example of a Blow-Up Ratio Calculation
Suppose a blown film production line uses a die with a diameter of 100 millimeters, and the inflated bubble has a diameter of 300 millimeters. Dividing 300 by 100 gives a blow-up ratio of 3, expressed as 3:1. This means the bubble diameter is three times the die diameter. If the bubble diameter increases to 350 millimeters while the die remains unchanged, the ratio becomes 3.5:1. This calculation helps operators translate bubble dimensions into a standardized process measurement and compare operating conditions across different production runs.
Calculating Blow-Up Ratio From Lay-Flat Width
Manufacturers frequently measure the lay-flat width of collapsed tubular film rather than the diameter of the inflated bubble. The lay-flat width is the width of the flattened tube, measured across its two joined layers. For an approximately circular bubble, its relationship to the blow-up ratio can be expressed as BUR = 2 × lay-flat width ÷ (π × die diameter). This alternative calculation is useful when the bubble is difficult to measure directly, but it assumes the tube is sufficiently circular and the lay-flat measurement is accurate. A flattened width of approximately 157 millimeters from a die measuring 100 millimeters corresponds to a blow-up ratio of approximately 1:1, while a width of approximately 471 millimeters corresponds to 3:1.
Why Is Blow-Up Ratio Important in Plastic Manufacturing?
The blow-up ratio helps manufacturers control the relationship between bubble expansion, film dimensions, and material orientation. During production, polymer chains become oriented as the molten film stretches in different directions, influencing the finished film’s mechanical behavior. The ratio also affects the achievable lay-flat width for a particular die and helps operators establish suitable processing conditions. However, the finished film’s performance depends on more than bubble diameter alone. Resin composition, melt temperature, cooling rate, drawdown, die design, and production speed all influence the final result. Using the blow-up ratio as one part of a wider process-control strategy can help manufacturers produce film that meets specified dimensional and performance requirements.
Influence on Film Width
Film width is one of the most direct outcomes of the blow-up ratio. Increasing the bubble diameter while keeping the die diameter constant increases the lay-flat width of the collapsed tube. This allows manufacturers to produce wider tubular film without necessarily installing a larger die. The relationship is particularly useful in packaging operations where different bag sizes or roll widths must be manufactured on the same production line. Nevertheless, operators must account for the collapsing frame, nip-roll alignment, bubble stability, and width tolerances to ensure that the finished film consistently meets the required dimensions.
Influence on Film Thickness
Blow-up ratio affects the distribution of polymer across the expanding film surface, but it does not determine thickness independently. At a given material output and suitable haul-off conditions, increasing the bubble diameter spreads the polymer across a larger surface area, generally reducing film thickness. However, changes in production speed, die gap, output rate, and material flow can also change the final gauge. Manufacturers therefore measure film thickness directly rather than assuming that a particular blow-up ratio guarantees a specified thickness. Consistent gauge control is especially important for packaging films, where excessive variation can affect sealing performance, material consumption, and product reliability.
Influence on Molecular Orientation
Molecular orientation describes how polymer chains become aligned during stretching and processing. In blown film extrusion, the blow-up ratio contributes to orientation in the transverse direction, while the haul-off process contributes to orientation in the machine direction. This directional alignment can affect tensile strength, stiffness, tear behavior, shrinkage, and other mechanical characteristics. The relationship is not identical for every polymer because different resin structures respond differently to heat, deformation, and cooling. Manufacturers must therefore evaluate the combined effects of transverse expansion and machine-direction drawing instead of relying on the blow-up ratio as a complete predictor of film performance.
What Is a Good Blow-Up Ratio?
There is no single ideal blow-up ratio for every blown film application. Suitable values depend on the polymer grade, die design, film thickness, desired width, production speed, cooling capacity, and required mechanical properties. Ratios around 2:1 to 3:1 are common in many polyethylene film applications, while certain materials and specialized production lines may operate at lower or higher values. Technical references describe broader operating ranges, sometimes extending from approximately 1.5:1 to 4:1 or beyond for particular applications. These figures are general examples rather than universal specifications. The appropriate target should be established using resin supplier recommendations, equipment limitations, product requirements, and controlled production trials.
Blow-Up Ratio for LDPE Film
Low-density polyethylene (LDPE) is widely used for flexible packaging, liners, and bags because of its flexibility and useful processing characteristics. Blow-up ratios around 2:1 to 3.5:1 are used in some LDPE film applications, although actual operating conditions vary by resin grade and equipment. The material’s melt behavior and ability to maintain a stable bubble influence the practical operating window. Manufacturers producing LDPE film should consider clarity, toughness, sealing requirements, thickness consistency, and bubble stability when selecting a ratio. A setting that performs well for one LDPE formulation may not deliver the same results with another grade or production configuration.
Blow-Up Ratio for HDPE Film
High-density polyethylene (HDPE) is used in applications such as shopping bags, liners, and thin packaging films that require a different balance of stiffness, strength, and material usage. Some high-molecular-weight HDPE blown film processes use comparatively high blow-up ratios, including values around 4:1 to 6:1, depending on resin characteristics and equipment design. These values should not be treated as standard targets for every HDPE line. The resin’s molecular structure, melt strength, cooling conditions, and desired film properties determine which ratios are practical. Operators should confirm that the selected setting produces a stable bubble and suitable mechanical performance before increasing production output.
Blow-Up Ratio for LLDPE Film
Linear low-density polyethylene (LLDPE) is frequently used for stretch films, heavy-duty bags, and packaging that requires good toughness and puncture resistance. Its processing behavior can differ from LDPE, particularly in relation to melt strength, surface defects, and bubble stability. A blow-up ratio around 2:1 to 3.5:1 may be suitable for some LLDPE applications, but the correct value depends on the formulation and production line. Manufacturers should evaluate film toughness, thickness uniformity, surface quality, and sealing performance when adjusting the ratio. Where LLDPE is blended with other polyethylene grades, the blend composition can further influence the operating window.
Blow-Up Ratio vs. Drawdown Ratio
Blow-up ratio and drawdown ratio describe different aspects of the stretching that occurs during blown film extrusion. The blow-up ratio measures expansion across the film’s width, whereas drawdown describes the reduction in thickness associated with pulling the molten polymer away from the die. In practical calculations, drawdown ratio is often expressed using the die gap, final film thickness, and blow-up ratio, subject to the assumptions of the chosen process model. Both ratios contribute to film orientation and thickness reduction. Evaluating them together gives manufacturers a more useful understanding of the process than considering either measurement in isolation.
Understanding Machine Direction and Transverse Direction
The machine direction (MD) is the direction in which the film travels through the production line, while the transverse direction (TD) runs across its width. During extrusion, haul-off speed influences stretching in the machine direction, and bubble inflation influences stretching in the transverse direction. The balance between these two forms of deformation can affect how the film responds to tension, tearing, and heat. For example, a film that performs well under tension along its length may behave differently when loaded across its width. Manufacturers must evaluate directional properties when developing packaging films for applications with specific strength, shrinkage, or converting requirements.
Why Both Ratios Matter
A suitable blow-up ratio cannot compensate for an unsuitable drawdown setting, and a suitable drawdown ratio cannot correct every problem caused by poor bubble control. Two production runs can use the same blow-up ratio yet produce films with different thicknesses and mechanical properties because their output rates, haul-off speeds, or die gaps differ. Similarly, changing the resin grade can alter the way a film responds to identical settings. Operators should assess the combined relationship between transverse expansion, machine-direction stretching, and final gauge. This approach makes troubleshooting more systematic and helps avoid adjustments that improve one characteristic while creating problems elsewhere.
Factors That Affect Blow-Up Ratio Performance
The practical performance of a blow-up ratio depends on several interacting variables. Even when the calculated ratio remains constant, changes in raw materials, extrusion temperature, cooling airflow, or equipment alignment can alter the finished film. Manufacturers must distinguish between the numerical ratio and the stability of the process used to achieve it. A reliable production setup maintains the intended bubble dimensions while controlling thickness variation, surface appearance, and mechanical properties. Understanding the following factors helps operators determine why a ratio works well under one set of conditions but produces defects under another.
Polymer Type and Melt Strength
The polymer’s melt strength describes its ability to resist deformation and support itself while molten. A resin with suitable melt strength can maintain a stable bubble during expansion, whereas an unsuitable material may sag, fluctuate, or rupture under demanding conditions. Molecular weight, molecular weight distribution, branching, and melt flow characteristics influence processability. LDPE, HDPE, and LLDPE therefore cannot always use identical settings, even when the desired film width and thickness are similar. Resin suppliers’ technical guidance is valuable when selecting an operating range, particularly when introducing a new grade or changing the proportions of a polymer blend.
Extrusion Temperature
Extrusion temperature affects polymer viscosity, melt flow, and the way the material responds to stretching. If the temperature profile is unsuitable for the resin, the bubble may become difficult to stabilize or the film may develop surface defects and inconsistent dimensions. Higher temperatures do not automatically improve production, just as lower temperatures do not automatically produce stronger film. The correct temperature depends on the polymer grade, screw design, output rate, and equipment configuration. Operators should use the recommended processing window and make controlled adjustments while monitoring melt pressure, bubble behavior, and finished-film quality.
Cooling and Frost Line Height
Cooling determines how quickly the expanded film solidifies and helps establish the point at which the bubble transitions from molten material to a more stable film. This transition is commonly associated with the frost line in polyethylene film production. Air-ring performance, airflow distribution, ambient conditions, and internal bubble cooling can influence the frost line and bubble stability. Uneven cooling may contribute to thickness variation, unstable dimensions, or inconsistent optical properties. Manufacturers should therefore monitor the cooling system when changing the blow-up ratio, since a ratio that is stable under one cooling configuration may become difficult to maintain under another.
Die Design and Equipment Stability
Die diameter, die gap, melt distribution, and equipment alignment all influence the quality of the blown film. A die with uneven flow around its circumference can create gauge variation even when the overall blow-up ratio is correct. Similarly, unstable haul-off equipment, poorly aligned nip rolls, or inconsistent cooling airflow can introduce defects unrelated to the ratio itself. Routine inspection and maintenance help maintain repeatable conditions. When a production line experiences persistent quality problems, operators should inspect the complete extrusion system instead of assuming that changing the bubble diameter will resolve the underlying cause.
Common Blow-Up Ratio Problems and Solutions
Problems associated with the blow-up ratio often become visible as changes in bubble shape, film width, thickness distribution, or finished-roll quality. The ratio is an important diagnostic measurement, but troubleshooting requires identifying the actual source of the defect. An operator should compare current settings with a known stable production setup, verify measurements, and adjust one relevant variable at a time whenever practical. This method helps reveal whether the problem originates in bubble expansion, material behavior, cooling, or mechanical equipment. The appropriate correction should always be confirmed through measurements of the finished film rather than judged by bubble appearance alone.
Unstable or Oscillating Film Bubble
An unstable bubble may move from side to side, change diameter, or develop periodic fluctuations that interfere with consistent production. Potential causes include unsuitable airflow, excessive expansion for the material, inconsistent melt output, drafts, and inadequate bubble stabilization. Operators should first check the cooling-air distribution, internal air supply, and stability of the extrusion output. They can then review the blow-up ratio against the resin’s recommended operating range. Reducing the ratio may help in some cases, but the correct response depends on the source of instability. Changing multiple settings simultaneously can make the problem harder to diagnose.
Uneven Film Thickness
Uneven gauge can occur when the bubble expands inconsistently, melt distribution is uneven, or cooling and haul-off conditions vary around the circumference. A correct average blow-up ratio does not guarantee uniform thickness across the entire film. Manufacturers should check the die gap, die cleanliness, air-ring alignment, bubble centering, and thickness measurements. They should also consider whether the output rate and haul-off speed are stable. Once the source of variation is identified, carefully controlled adjustments can improve uniformity. For demanding applications, continuous gauge monitoring can help detect deviations earlier than occasional manual checks.
Wrinkles and Poor Film Appearance
Wrinkles can develop during bubble collapsing, film handling, or winding, and are not necessarily caused by an incorrect blow-up ratio. An unsuitable ratio may contribute to bubble instability or changes in film orientation, but misaligned nip rolls, collapsing-frame settings, uneven cooling, and winding tension can also be responsible. Poor clarity or surface appearance may have additional causes, including resin properties, frost line conditions, and melt-related defects. Manufacturers should determine where the defect first appears and inspect the corresponding equipment and process conditions. Correcting the underlying issue is more reliable than repeatedly adjusting the ratio without supporting evidence.
Applications of Blow-Up Ratio in Industry
The blow-up ratio is relevant wherever tubular plastic film is manufactured through a blown film extrusion process. Packaging manufacturers use it to help establish the dimensions and processing conditions needed for bags, flexible wrapping, and protective liners. Agricultural film producers may use blown film equipment to manufacture covers and other plastic sheeting, while industrial manufacturers use the process for films designed around particular handling and protection requirements. The precise operating conditions differ by product, resin, equipment, and performance specification. In each case, the ratio provides a common way to describe transverse expansion and support communication between production teams, engineers, and quality-control personnel.
Plastic Bags and Flexible Packaging
Plastic bags and flexible packaging require consistent dimensions, appropriate thickness, and suitable strength for their intended use. Blow-up ratio helps determine the width of tubular film produced from a particular die, making it useful when planning production for different bag sizes. However, a bag’s performance also depends on resin selection, film gauge, sealing conditions, and converting operations. Manufacturers should confirm that the film meets its specifications after extrusion and bag conversion. For food-contact packaging, applicable material and regulatory requirements must also be considered independently of the chosen blow-up ratio.
Agricultural and Industrial Films
Agricultural films and industrial liners may require specific combinations of width, durability, flexibility, and environmental resistance. The blown film process can produce large continuous tubes that are later converted into products suited to these uses. The selected blow-up ratio affects the achievable dimensions and contributes to film orientation, but other factors determine whether the finished product meets its performance requirements. Outdoor applications, for example, may also require appropriate resistance to ultraviolet exposure and environmental degradation. Manufacturers must evaluate the complete formulation and finished-film properties rather than assuming that a particular expansion ratio provides these protections.
Best Practices for Optimizing Blow-Up Ratio
Optimizing the blow-up ratio starts with defining the required finished-film width, thickness, and mechanical properties. Manufacturers should select a compatible resin and die configuration, establish a stable baseline, and confirm the actual bubble diameter or calculate it from a reliable lay-flat measurement. Changes should be made gradually, with production records maintained for the ratio, temperature profile, output rate, haul-off speed, cooling conditions, and final gauge. This information allows operators to compare successful runs and identify recurring problems. The best operating setting is the one that consistently meets the product specification while maintaining stable production, acceptable material usage, and the required output rate.
Monitor Quality Rather Than Chasing a Higher Ratio
A higher blow-up ratio is not automatically better. Increasing it can help produce a wider film from a given die, but it may also change molecular orientation and place additional demands on bubble stability. The resulting mechanical properties depend on the resin and the other processing conditions. Manufacturers should evaluate the finished film using appropriate measurements, such as thickness uniformity, tensile properties, tear resistance, optical quality, and dimensional consistency where relevant. The target ratio should reflect the intended application and validated process conditions rather than an assumption that maximum expansion will deliver the best result.
Document and Validate Process Changes
Consistent production benefits from recording the conditions associated with acceptable film quality. When a new resin, die, or product specification is introduced, controlled trials can help establish a suitable operating range. Operators should document both the settings and the measured outcomes, including any defects or deviations. Repeating successful conditions provides a practical starting point for future production, although adjustments may still be necessary when materials or equipment change. For specialized films, technical consultation with the resin supplier or equipment manufacturer can help determine whether a proposed ratio falls within the recommended processing window.
Conclusion
The blow-up ratio is a fundamental parameter in blown film extrusion because it connects the extrusion die diameter with the expanded bubble diameter and helps manufacturers control film width and transverse stretching. Its influence extends to thickness, molecular orientation, mechanical properties, and production stability, but it must be evaluated alongside drawdown, resin characteristics, cooling, and equipment conditions. There is no universally ideal ratio for every polymer or application. By using the correct calculation, selecting suitable processing conditions, and validating results through finished-film measurements, manufacturers can improve dimensional consistency and produce films that meet their intended performance requirements.
FAQs
1. What is the blow-up ratio in plastic manufacturing?
The blow-up ratio measures the expanded film bubble diameter divided by the extrusion die diameter, indicating how much the molten plastic tube expands transversely.
2. How do you calculate the blow-up ratio?
Divide the bubble diameter by the die diameter using identical units. For example, a 300-millimeter bubble and 100-millimeter die produce a 3:1 ratio.
3. What is a normal blow-up ratio for polyethylene film?
Many polyethylene applications use ratios around 2:1 to 3:1, although suitable settings vary with resin grade, equipment, thickness, and product requirements.
4. Does a higher blow-up ratio improve film strength?
Not necessarily. Higher ratios change transverse molecular orientation, but final strength depends on polymer type, drawdown, cooling, film thickness, and other processing conditions.
5. What is the difference between blow-up ratio and drawdown ratio?
Blow-up ratio describes transverse bubble expansion, while drawdown ratio describes longitudinal stretching and thickness reduction as molten film moves through the production line.
6. How can manufacturers fix blow-up ratio problems?
Manufacturers should check bubble stability, cooling airflow, die alignment, resin properties, and film thickness before making controlled adjustments and verifying finished-product quality.
More read: Hypackel